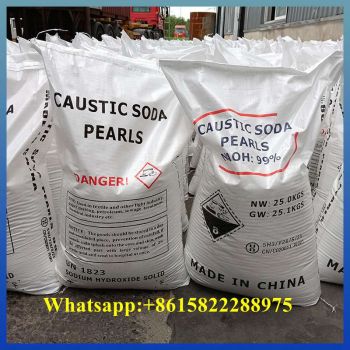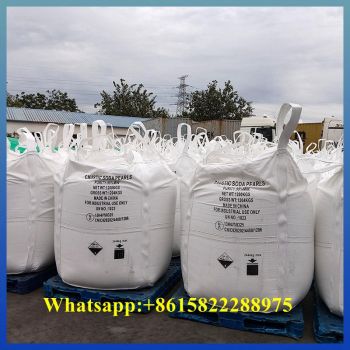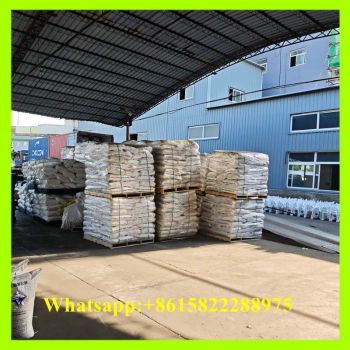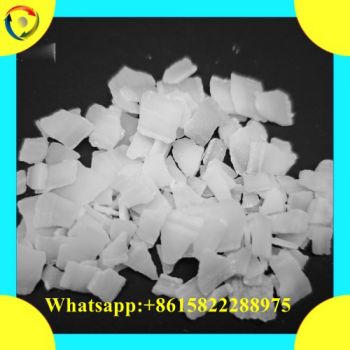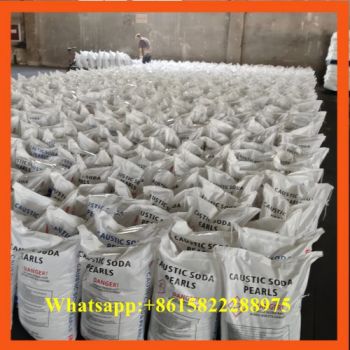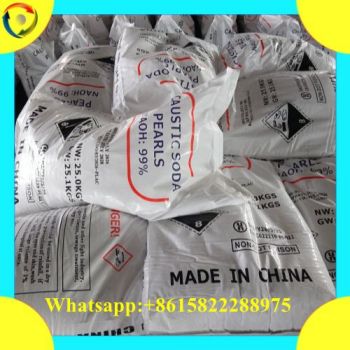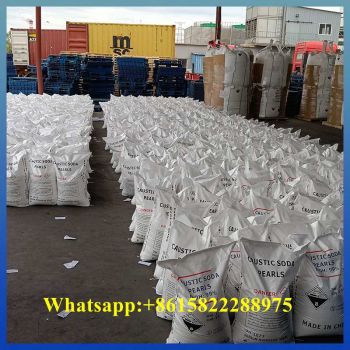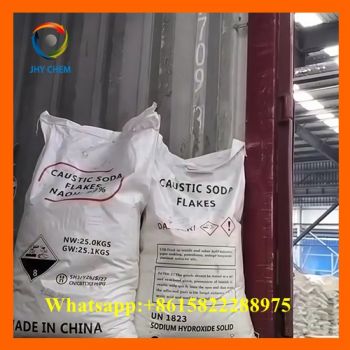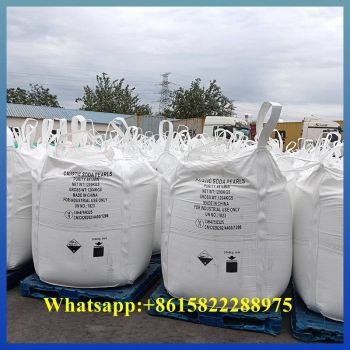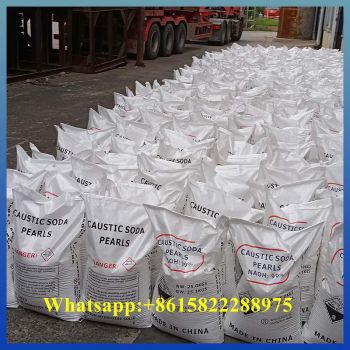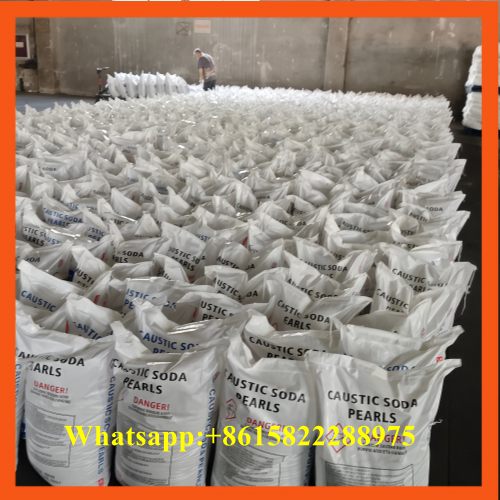


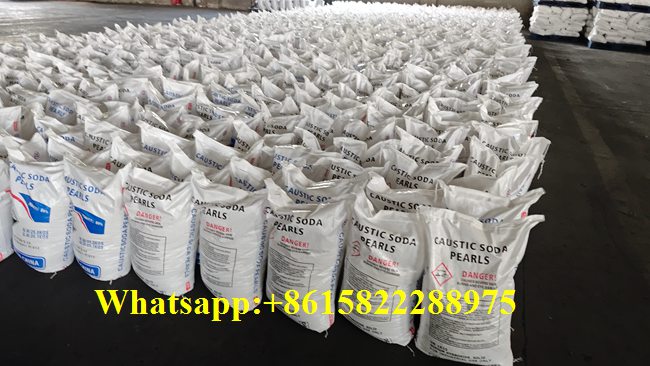
Optimizing material handling efficiency and safeguarding chemical integrity throughout international maritime transit requires specialized packaging engineering paired with high-purity chemical manufacturing. As an established chlor-alkali producer supplying global manufacturing hubs, our factory provides high-grade 25kg caustic soda formulated at a certified minimum chemical purity of 99%. Designed specifically for large-scale industrial buyers, mining operations, detergent plants, and chemical distributors, our standardized packaging system prevents atmospheric degradation while providing uniform unit weights for effortless warehouse management and inventory control.
Operating with a total annual production capacity of 120,000 metric tons, we maintain scheduled containerized exports to major commercial seaports across Latin America, Southeast Asia, the Middle East, Europe, and Africa. By operating a direct manufacturer-to-buyer distribution model, we eliminate trading company markups, enabling your procurement team to secure full container load (20ft FCL) shipments at competitive factory-direct wholesale pricing.
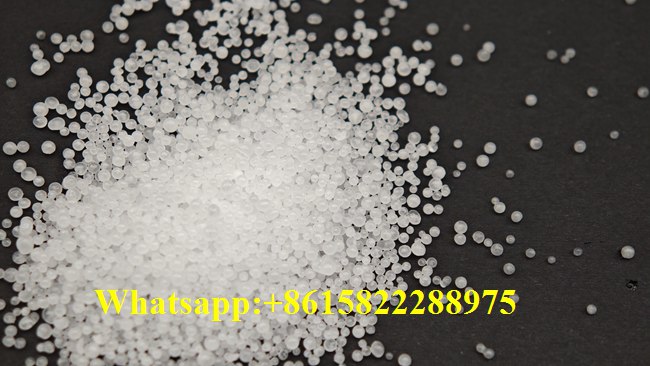
| Composing | Flake/pearl/solid 96% | Flake/pearl/solid 98% | Flake/pearl/solid 99% |
| NaOH | 96% Min | 98% Min | 99% Min |
| Na2CO3 | 1% Max | 0.5% Max. | 0.4% Max. |
| NaCl | 2% Max. | 0.03% Max. | 0.015% Max |
| Fe203 | 0.01% Max | 0.005% Max | 0.001% Max |
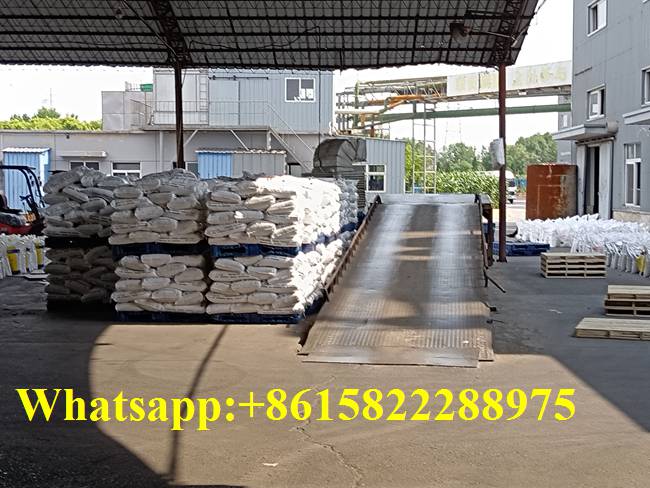
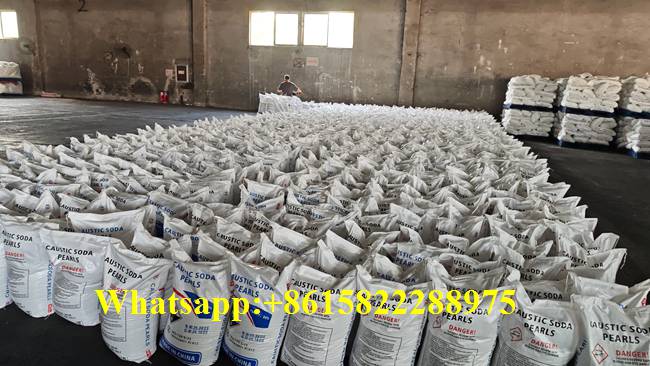
Transporting hygroscopic chemicals across varying climate zones and tropical sea routes demands rigorous moisture barrier protection. Every shipment of our 25kg caustic soda utilizes a reinforced packaging architecture built for harsh ocean transit:
1. Heavy-Duty Polypropylene (PP) Outer Bag: A high-tensile woven outer shell that protects against mechanical abrasion, tearing, and puncture hazards during automated loading, forklift transport, and warehouse stacking.
2. Hermetically Sealed Polyethylene (PE) Inner Liner: An airtight inner plastic film forming an absolute barrier against atmospheric moisture, humidity, and carbon dioxide absorption, effectively preventing product caking or premature degradation.
3. Standardized Unit Weight: Offers an ideal balance between manual handling convenience for plant operators and high-density palletization for maximum storage efficiency.
Our export-grade chemical inventory is engineered to meet stringent technical standards across a broad spectrum of heavy manufacturing industries:
● Soap and Detergent Manufacturing: Serves as a vital saponification agent for vegetable oils and tallow, ensuring firm soap bar consistency and high-foaming industrial cleaners.
● Mining and Hydrometallurgy: Essential for gold, alumina, and base metal extraction, providing consistent pH elevation for froth flotation and leaching circuits.
● Water Treatment and Environmental Protection: Neutralizes acidic industrial wastewater streams, municipal water supplies, and heavy metal precipitation units.
● Textile and Paper Processing: Facilitates wood pulp digestion, cotton mercerization, and fabric scouring operations.
Strategically located just 15 kilometers from Tianjin Port, our chemical production complex ensures rapid inland delivery and priority vessel loading. Our dedicated export documentation department manages all required customs paperwork to guarantee smooth entry at destination ports, including lot-specific Certificates of Analysis (COA), Globally Harmonized System (GHS) compliant Safety Data Sheets (SDS), and required regional tracking waivers or pre-shipment inspection certificates.
Every production lot undergoes comprehensive laboratory testing prior to dispatch, with third-party inspection verification available upon request from international agencies such as SGS, Bureau Veritas, or Intertek. Contact our commercial sales team today to request custom export quotations or reserve full container load (FCL) shipments tailored to your operational schedule.
Tel:+86-22-66863746
Fax:+86-22-66863746 ext. 608
Mobile Phone:
+86-15822288975(WhatsApp)
E-mail: causticsoda@jiahengyuanchem.com
Add:NO.1023, 10F, BLDG B, JUNJING SQUARE, HANGYUN 1ST ROAD, TEDA, TIANJIN, CHINA