In today’s fast-paced industrial manufacturing landscape, maintaining uninterrupted factory operations relies heavily on a resilient, transparent supply chain. Fundamental chemical building blocks, particularly high-purity sodium hydroxide (NaOH ≥ 99%), form the chemical foundation for countless downstream processing workflows worldwide. Unpredictable variations in chemical purity or delayed delivery schedules can lead to costly operational downtime, reduced product yields, and compromised finished goods.
When global procurement managers partner with experienced raw chemicals suppliers operating integrated chlor-alkali manufacturing facilities, they secure direct access to large-scale output capabilities, strict lot-to-lot consistency, and streamlined maritime logistics. This direct-from-factory collaboration minimizes procurement risk, hedges against spot market volatility, and ensures a steady supply of essential alkaline reagents.

Sourcing from verified primary producers guarantees that high-purity reagents meet the rigorous technical standards demanded across heavy industrial processing sectors:
● Water Purification and Effluent Conditioning: Acts as a powerful alkalizing agent for precise pH neutralization and the effective precipitation of toxic heavy metals in municipal and industrial wastewater streams.
● Soap and Commercial Cleaning Formulations: Provides the essential strong alkaline base required for the efficient saponification of natural fats and oils into high-grade soaps and industrial degreasers.
● Pulp, Paper, and Fiber Processing: Facilitates wood fiber separation and lignin removal during advanced Kraft delignification and pulp bleaching phases.
● Textile Wet-Processing and Mercerization: Swells natural cotton fibers to permanently enhance fabric luster, tensile strength, and dyestuff absorption capacity.
● Mining and Extractive Metallurgy: Regulates alkalinity in complex mineral slurry circuits, gold recovery leaching processes, and bauxite alumina refining.

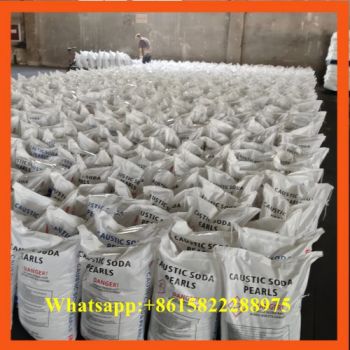
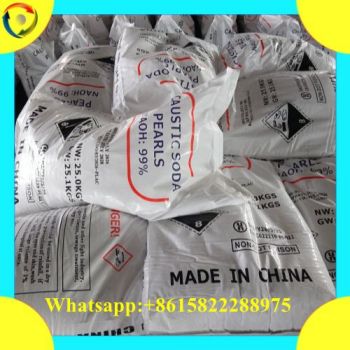
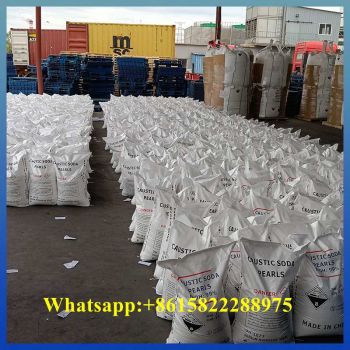
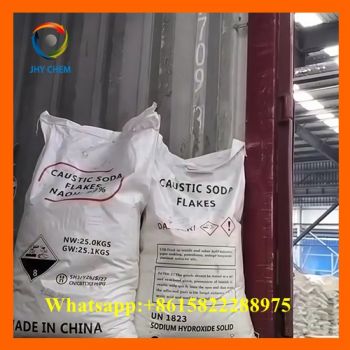
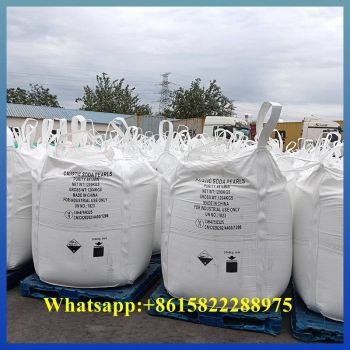
Anhydrous solid sodium hydroxide is intensely hygroscopic, rapidly absorbing atmospheric moisture and carbon dioxide if exposed. Preserving active chemical potency during transoceanic transit and extended tropical warehouse storage requires heavy-duty barrier packaging engineered to strict international transport safety standards:
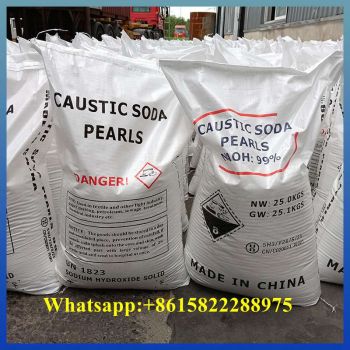
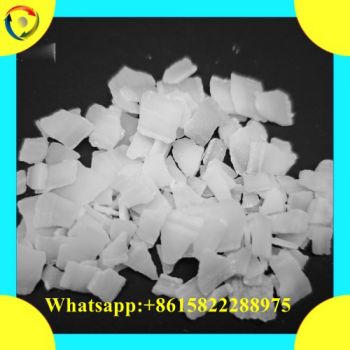
1. Hermetic Polyethylene (PE) Inner Liner: A thick internal plastic film heat-sealed to isolate solid flakes or micro-pearls completely from sea air, ambient humidity, and condensation.
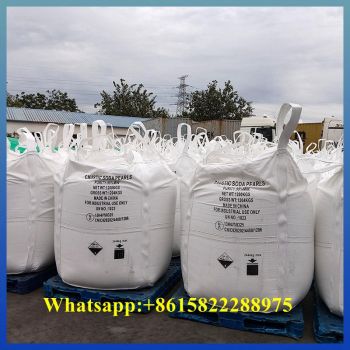
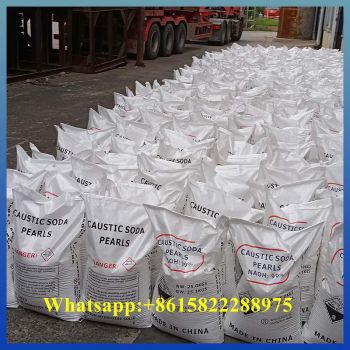
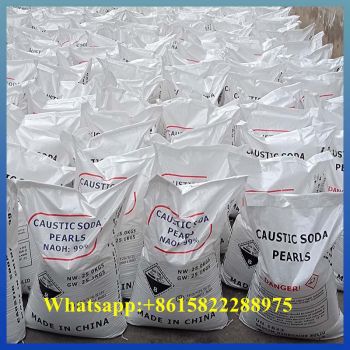
2. High-Tenacity Polypropylene (PP) Woven Outer Bag: A rugged external shell engineered to provide high tensile strength and puncture resistance against mechanical stress during port loading and container stacking.
3. Ergonomic 25kg Standard Weight: Complies fully with international occupational health standards, facilitating safe manual handling, accurate batch weighing, and zero-loss hopper feeding.
Evaluating dependable raw chemicals suppliers requires looking beyond basic baseline quotations to verify origin transparency, Quality Assurance (QA) protocols, and international trade compliance. Purchasing directly from a primary chlor-alkali producer eliminates unnecessary trading markups, optimizes freight shipping schedules, and guarantees complete product origin traceability.
Every export batch undergoes rigorous pre-shipment laboratory analysis. All dispatches are accompanied by a complete trade documentation package, including a lot-specific Certificate of Analysis (COA), Globally Harmonized System (GHS) compliant Safety Data Sheets (SDS), and UN-certified packaging documentation for Class 8 hazardous corrosive solids (UN 1823). Contact our international commerce team today to request technical data sheets, order evaluation samples, or schedule custom Full Container Load (FCL) shipments tailored to your factory timeline.
Tel:+86-22-66863746
Fax:+86-22-66863746 ext. 608
Mobile Phone:
+86-15822288975(WhatsApp)
E-mail: causticsoda@jiahengyuanchem.com
Add:NO.1023, 10F, BLDG B, JUNJING SQUARE, HANGYUN 1ST ROAD, TEDA, TIANJIN, CHINA